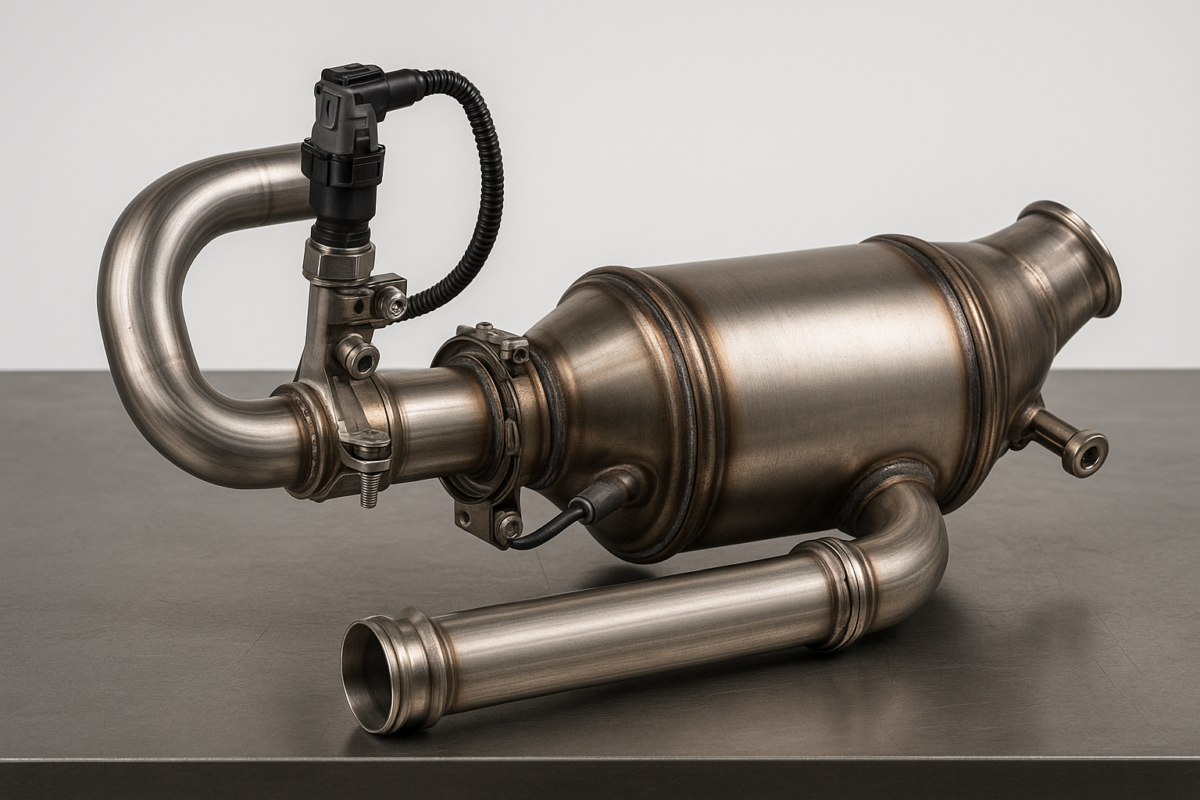
What DEF Crystallization Actually Is
Diesel exhaust fluid is a precisely engineered solution: 32.5% urea by weight dissolved in 67.5% deionized water. That ratio is not a marketing target — it’s the exact eutectic composition that gives DEF its ISO 22241 properties, its lowest freezing point (about 12°F / -11°C), and its predictable behavior when injected into a hot SCR exhaust stream. Move outside that ratio in either direction and the chemistry stops cooperating.
Crystallization is what happens when the urea fraction of that solution falls out of liquid suspension and reverts to a solid. Inside the SCR system the process looks like this: liquid DEF leaves the injector tip as a fine spray, the water fraction flashes off as steam, the urea fraction thermally decomposes into ammonia (NH₃) and isocyanic acid (HNCO), and the ammonia reduces NOx across the catalyst into harmless nitrogen and water. That’s the chemistry working correctly.
Crystallization is the chemistry working incorrectly. Instead of cleanly vaporizing, some fraction of the urea cools below its decomposition temperature, recombines with HNCO and water on a nearby metal surface, and forms a hard deposit. The deposits are mainly cyanuric acid, biuret, melamine, and ammelide — secondary urea-derivative compounds that form when urea is heated to the wrong temperature for the wrong amount of time. Chemists call this family of byproducts “urea deposits.” Diesel technicians just call them “crystals.”
The first generation of these deposits is soft and white — almost like dried table salt. They can be wiped off with a rag if you catch them early. But each subsequent heat cycle bakes the deposit harder. By the time the layer is two or three millimeters thick, it has the hardness of porcelain and the bond strength of mild epoxy. At that point, you no longer wipe it off; you replace the part it’s attached to.
The economically important thing about urea crystallization is that the deposit doesn’t just sit there as a cosmetic nuisance. It actively interferes with three things the SCR system has to do correctly to stay legal: meter DEF in precise quantities (now blocked by deposits at the injector), atomize that DEF into a fine spray (now disrupted by deposits on the spray cone), and expose all of that decomposed ammonia to the catalyst face (now blocked by deposits on the substrate). When all three of those degrade simultaneously — which they always do, because the failure modes are linked — the engine’s NOx output drifts out of spec, the OBD system flags it, and the truck enters derate.
Where Crystals Form Inside the SCR System
Crystallization is not random. It forms at predictable locations inside the aftertreatment, each driven by specific thermal conditions. Understanding the geography of the deposits is the first step to understanding why they happen.
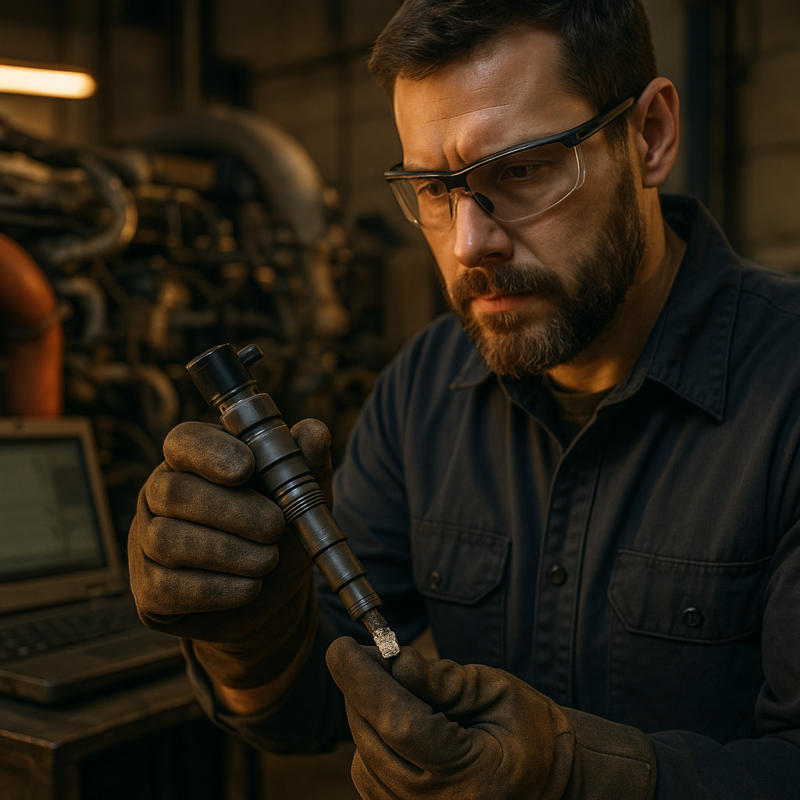
1. The DEF injector tip. This is the single most common crystallization site on the entire SCR system. The injector tip lives in a brutal thermal environment — it has to deliver liquid DEF at ambient temperature into an exhaust stream that’s between 400°F and 1,000°F. Every time the engine shuts down, residual DEF in the injector tip is exposed to soak-back heat from the exhaust pipe. The water evaporates, the urea concentrates, and the next cold start has to push fresh DEF past a thin crust of dried urea. Over thousands of cycles, that crust grows from invisible to thick enough to deflect the spray pattern.
2. The decomposition tube (or “DEF doser tube”). Downstream of the injector, the spray cone has a defined geometry — it’s engineered to atomize and partially vaporize before reaching the mixer. If the spray hits the tube wall instead of staying in suspension (because the injector pattern has been deflected by crystals, or because temperatures are too low for clean vaporization), urea deposits build on the tube interior. These deposits are usually visible during a borescope inspection as a white or yellowish crust on the inside surface.
3. The mixer. Most modern SCR systems use a swirl mixer — a vaned device that turbulates the exhaust stream to distribute ammonia evenly across the catalyst inlet. The mixer is also the place where the last fraction of incompletely decomposed urea tends to land. Crystals on the mixer vanes are particularly destructive because they disrupt the flow distribution across the catalyst, creating “hot lanes” and “cold lanes” of ammonia that the catalyst can’t compensate for.
4. The catalyst face (substrate inlet). The face of the SCR catalyst — the upstream cross-section of the substrate — is the worst place for crystals to form, because they directly block the active surface area where NOx reduction happens. Crystallized urea on the catalyst face is also chemically aggressive over time, masking active sites and forming sintered layers that resist cleaning. Once the face is heavily fouled, catalyst replacement is usually the only practical fix.
5. The DEF tank header and supply line. Less frequently discussed: the DEF tank header (which contains the level sensor, temperature sensor, and supply pickup) can accumulate deposits if the DEF being used is contaminated or off-spec. A clogged supply line strainer or fouled header sensor will throw its own set of fault codes — usually quality codes (P204F, P203D) — long before catalyst-face crystallization is visible.
6. The NOx sensors. Both the upstream and downstream NOx sensors live in the exhaust stream and are vulnerable to surface contamination. While they’re not “crystallizing” in the urea-deposit sense, contaminated DEF or upstream crystal sloughing can poison the sensor element, causing false readings that trigger SCR-efficiency faults. NOx sensor replacement runs $400–$900 per sensor.
Why Crystallization Happens — Six Root Causes
Crystallization is rarely caused by a single failure. It’s almost always a stack of small contributing factors that compound over time. Six common root causes:
1. Thermal cycling at the injector tip. Every engine shutdown and restart cycles the injector tip through a temperature range that favors crystal nucleation. A truck that runs continuous long-haul has fewer crystallization events than a truck that runs short urban routes with many starts and stops, even if total DEF consumption is identical. Delivery vans, stop-and-go construction equipment, and short-route fleet trucks are at higher crystallization risk than OTR Class 8 semis.
2. DEF concentration drift in storage. DEF is a 32.5% urea solution. If it sits in a partially-full storage tank with the bung loose, the water fraction evaporates first, leaving the urea more concentrated than spec. A drum that started at 32.5% urea can drift above spec after months of warm storage with poor sealing. That over-concentrated DEF behaves badly in the SCR — it deposits aggressively because the chemistry is already biased toward precipitation.
3. Contamination — diesel, dust, salt, fingertips. DEF is supposed to be ultra-pure. ISO 22241 specifies maximum limits on iron, copper, zinc, calcium, sodium, magnesium, and several other ions because trace metals catalyze unwanted side reactions in the SCR system. Real-world contamination usually enters DEF through three pathways: dirty transfer equipment (a pump or hose that touched diesel or hydraulic fluid), unsealed storage exposed to atmospheric dust, or hands and rags that introduce skin oils and salt. Contaminated DEF accelerates crystallization dramatically — and the contamination is usually invisible to the naked eye.
4. Low duty cycle / extended low-temperature operation. SCR catalysts have a minimum operating temperature below which the urea-to-ammonia decomposition doesn’t complete cleanly. Trucks that idle excessively, equipment that runs at low load for long periods (standby generators, low-speed agricultural Tier 4 tractors), or systems that operate in deep cold-weather conditions tend to leave partially-decomposed urea in the system. That partial decomposition is the chemical precursor to crystallization.
5. Cold restarts with residual DEF in the system. When a hot engine shuts down on a cold day, the DEF lines and injector cool through the precipitation window before fully purging. The next morning’s cold start has to push fresh DEF past whatever solidified overnight. Modern systems have a purge cycle at shutdown to address this, but the purge isn’t perfect — particularly on older OEM platforms or on systems where the DEF pump has degraded.
6. Sub-spec DEF — the cheap-pump-at-the-fuel-island problem. Not all DEF sold at retail meets ISO 22241. Bulk DEF dispensed from poorly maintained pumps can carry biofilm, mineral contamination from the holding tank, or simply be diluted with water by an unscrupulous operator. DEF that reads below the 31.8% lower urea limit in ISO 22241-1, or carries metal contamination, is a crystallization accelerator from the moment it enters the truck.
The Real Cost of Crystallization by Repair Tier
Crystallization is a tiered failure — each level of severity has a different repair signature and a different price tag. The economic argument for prevention lives in this table:
Tier 1: DEF injector replacement. Cost range: $400 to $1,500 per event. The DEF injector itself runs $250–$900 depending on platform (a 6.7 Cummins injector is on the low end; a Detroit DD15 injector is on the high end). Labor is 1–2 hours at $150–$200/hour. This is the cheapest crystallization repair because the injector is designed to be a replaceable wear item — it doesn’t require removing the catalyst housing. Most light-duty platforms see this repair first.
Tier 2: Decomposition tube / mixer cleaning or replacement. Cost range: $800 to $2,500 per event. If crystals have migrated past the injector into the decomposition tube and mixer, the repair gets more involved. Cleaning is sometimes possible (chemical soak or careful mechanical removal), but if the deposits are sintered, the mixer assembly often gets replaced as a unit. This repair tier is more common on Class 8 trucks and on equipment with high crystallization mileage that wasn’t caught at Tier 1.
Tier 3: SCR catalyst cleaning. Cost range: $1,200 to $3,500 per event. Specialized SCR cleaning services use chemical baths and controlled high-temperature regen cycles to dissolve crystallized deposits from the catalyst face. Done correctly, this restores most of the catalyst’s NOx-reduction capacity. Done incorrectly (with aggressive caustic chemistry, mechanical scraping, or excessive heat), it permanently damages the active coating. The catalyst-cleaning industry is uneven in quality — choose a service with documented before-and-after testing.
Tier 4: SCR catalyst replacement. Cost range: $3,500 to $8,000 on light-duty pickups and Class 8 trucks; $8,000 to $35,000 on industrial generators and Tier 4 agricultural equipment. The catalyst itself runs $2,000–$25,000 depending on platform. Labor is 4–10 hours. Disposal of the old catalyst is regulated (the catalyst can contain metals that have to be handled or reclaimed under local rules). This is the worst-case crystallization outcome on most diesel platforms — the system has been allowed to degrade far enough that the catalyst can no longer be salvaged.
Tier 5: Cascading downstream damage. Cost range: highly variable, often $5,000–$25,000+ per event. Severe long-term crystallization can damage the NOx sensors, the DEF supply pump, the DEF level sensor, and in rare cases the upstream DPF (because forced regens triggered by SCR failure can over-cycle the DPF). At this level the repair becomes a system-level rebuild rather than a single component replacement.
The downtime multiplier. The parts-and-labor cost is only half the bill. Every crystallization repair takes the truck or piece of equipment out of service. For an owner-operator Class 8 hauler grossing $800–$2,400 per day, a 5-day repair window is $4,000–$12,000 in lost revenue on top of the repair invoice. For a fleet, the downtime cost compounds across multiple trucks if the same root cause (e.g., contaminated bulk DEF from one fuel island) is causing crystallization across the fleet simultaneously. For a hospital standby generator that fails an annual load test because of SCR crystallization, the cost includes compliance penalties and emergency-service callouts that can dwarf the underlying repair.
Platform-Specific Patterns: Cummins, Duramax, Powerstroke, Detroit, Cat
Crystallization affects every modern SCR-equipped diesel, but the patterns and economics differ meaningfully by platform. Here are the patterns to watch for on common platforms:
6.7 Cummins (Ram HD, medium-duty applications). The 6.7 Cummins has a large install base, and crystallization at the DEF injector tip is a common complaint. A typical symptom sequence: an initial P20EE code that clears, recurring codes every few thousand miles, and eventually a derate that won’t clear. See our dedicated 6.7 Cummins DEF Crystallization Guide. Cost of the typical 6.7 Cummins injector replacement: $450–$700. SCR cleaning if it progresses: $1,800–$2,800. Full catalyst replacement: $4,500–$6,500.
6.6 Duramax (GM HD). On the Duramax, DEF problems often show up as DEF system codes such as P204F (SAE J2012: Reductant System Performance) before injector deposits are found. The upstream sensors and the DEF pump assembly are sensitive to contamination. Short urban routes with high start-stop cycling raise the risk. Injector replacement: $400–$650. Full SCR system service: $3,500–$6,000.
6.7 Powerstroke (Ford Super Duty). The injector and decomposition tube accumulate deposits over time, so start at the injector when crystallization is suspected. Injector replacement: $500–$800. Catalyst replacement: $5,500–$7,500.
Detroit DD13 / DD15 / DD16 (Class 8 OTR semis). Detroit DD-series engines are the platform where crystallization economics get severe. The catalyst assemblies are large, expensive, and labor-intensive to replace. Left untreated, crystallization can progress through the tiers above. DD15 injector replacement: $900–$1,400. Full SCR catalyst replacement: $6,000–$8,500.
Cat C13 / C15 (heavy on-highway and off-highway). Cat platforms — both on-highway truck applications and off-highway construction and mining — share the Detroit pattern: large catalyst assemblies, expensive replacements, and high downtime cost per event. Cat C15 SCR catalyst replacement on a continuous-duty application can reach $12,000–$18,000 including labor. Off-highway applications are particularly vulnerable because of low duty cycle operation (extended idling at temperatures below the SCR operating window).
Agricultural Tier 4 Final platforms (John Deere PowerTech, Case IH FPT, AGCO Sisu). Agricultural equipment is highly exposed to crystallization because the duty cycle works against it — long periods of medium-load operation at temperatures right at the SCR threshold, then long winter storage with residual DEF in the system, then dusty operating conditions that contaminate any DEF stored on-farm. Catalyst replacement on a 200–400 HP tractor SCR: $4,500–$12,000. Combine and self-propelled sprayer SCR: $8,000–$22,000.
Prevention: Clean DEF, Storage Discipline, NüDef Chemistry
Crystallization prevention is built on three pillars. Skip any one and the other two can’t fully compensate.
Pillar 1: Use clean, ISO 22241-compliant DEF from the start. Buy DEF in sealed containers (totes, drums, or properly sealed bulk tanks) from a supplier who can show you the certificate of analysis. Avoid DEF dispensed from poorly maintained third-party pumps, especially the cheap unbranded ones at small fuel stops. If you operate a fleet large enough to consume DEF in bulk, get a relationship with a regional DEF distributor who can deliver to a dedicated on-site tank and certify each delivery against ISO 22241 specifications. Paying a little more for verified DEF costs far less than one crystallization repair event.
Pillar 2: Storage discipline. DEF degrades with temperature and exposure to atmosphere. The storage rules:
- Keep DEF below 86°F (30°C) for long-term storage. Above that, shelf life shortens dramatically.
- Keep DEF above its freezing point (about 12°F / -11°C). Freezing doesn’t destroy DEF — it can thaw and be used — but repeated freeze-thaw cycles can stratify the urea concentration.
- Keep containers sealed. Once open, DEF starts absorbing moisture from humid air and offgassing ammonia. Partially-used containers should be resealed promptly and consumed within months, not years.
- Never transfer DEF with a pump, hose, or container that has touched any other fluid. Diesel contamination, even in trace amounts, is a major crystallization accelerator.
- Don’t store DEF in direct sunlight, and don’t store it in containers other than the original or a DEF-certified replacement.
For fleets, this usually means installing a dedicated DEF storage tank (steel or HDPE, with a sealed bung and a clean pickup), keeping it in a temperature-controlled location, and refusing to share dispensing equipment with any other fluid. The discipline pays for itself the first time it prevents a crystallization event.
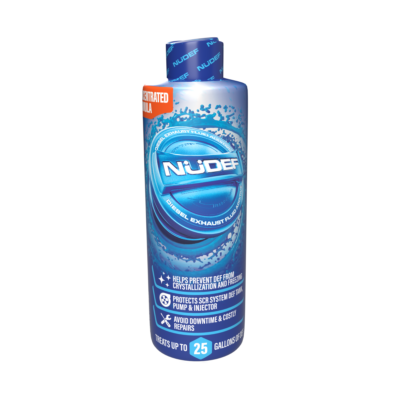
Pillar 3: Treat the DEF with NüDef. Clean DEF and good storage handle most of the prevention work, but they don’t address the thermal cycling that drives injector-tip crystallization on real-world duty cycles. NüDef DEF Treatment, Additive & Stabilizer is a DEF stabilizer and anti-scaling agent. One 8.45 fl oz bottle treats 25 gallons of DEF. Add it to the DEF tank at every refill and do not exceed the recommended dose.
What the NüDef label says it does:
- Helps prevent DEF crystallization
- Helps protect the SCR system, DEF tank, pump and injector
- Helps avoid downtime and costly repairs
- Helps prevent freezing (sell sheet)
For fleet wholesale pricing call (855) 300-0031.
When Crystallization Is Already Advanced — Clean or Replace?
Prevention is the right answer if you start before the first fault code. But what if you’re reading this because you already have a derate, recurring codes, or a service-write-up that says “SCR crystallization confirmed”? The decision tree:
Step 1: Read the codes and confirm the failure mode. Plug in a scan tool capable of reading the SCR-related fault codes:
- P20EE / P20EF: SCR NOx catalyst and pre-catalyst efficiency below threshold, bank 1 (SAE J2012). Catalyst-face crystallization is one possible cause.
- P207F: Reductant quality performance. Can indicate contaminated DEF or sensor-related issues.
- P204F: Reductant System Performance (SAE J2012). Often points to a DEF supply problem rather than catalyst damage.
- P20E8 / P20E9: DEF pressure low/high. Points to injector or pump-related issues, often crystallization-driven.
Confirm the diagnosis with a borescope inspection of the injector tip and decomposition tube. If you can see crystallized deposits, you have a Tier 1 or Tier 2 problem. If the injector and tube look clean but the codes persist, the catalyst face itself may be the issue.
Step 2: Determine the severity.
- If the injector tip has visible crystals but the system clears codes after a regen and a tip cleaning: Tier 1 intervention — clean or replace the injector, then start treatment immediately to prevent recurrence.
- If the decomposition tube and mixer have deposits but the catalyst face appears clean on inspection: Tier 2 intervention — clean or replace the affected components, start treatment, recheck within 5,000 miles.
- If the catalyst face has visible heavy deposits but the substrate appears structurally intact: Tier 3 intervention — specialist SCR cleaning service. Verify the service has documented before-and-after NOx-efficiency testing.
- If the catalyst substrate is structurally compromised (visible damage, severe sintering, or unable to recover NOx-reduction performance after professional cleaning): Tier 4 — catalyst replacement.
Step 3: Address the root cause before returning to service. Replacing the part without fixing the underlying cause means the new part will crystallize on the same timeline as the old part. The post-repair checklist:
- Drain and flush the DEF tank. The DEF that was in there is suspect — either contaminated, off-spec, or both. Refill with verified clean DEF.
- Inspect the DEF storage source. If you have an on-site bulk tank, sample it and test concentration. If you’ve been buying DEF from a third-party retail pump, change suppliers.
- Start treatment with NüDef on the fresh DEF fill. Treatment helps prevent new crystallization, and it works best on a clean system with fresh DEF.
- Recheck fault codes at 1,000 miles and again at 5,000 miles. If they recur, the root cause was not fully addressed and the diagnosis needs to be revisited.
Comparison: Crystallization Risk and Prevention by Scenario
The table below summarizes the main crystallization risk in common operating scenarios and the prevention steps that fit each one.
For deeper coverage on the cost side of this equation, see our Cost of Untreated DEF analysis. For platform-specific patterns on the most affected platform, see the 6.7 Cummins DEF Crystallization Guide. To see what a DEF additive can and cannot do, read Does DEF Additive Work? and our DEF additive guide.
For individual purchase visit nudef.com. For fleet pricing or wholesale account inquiries call (855) 300-0031 or email info@nudef.com.